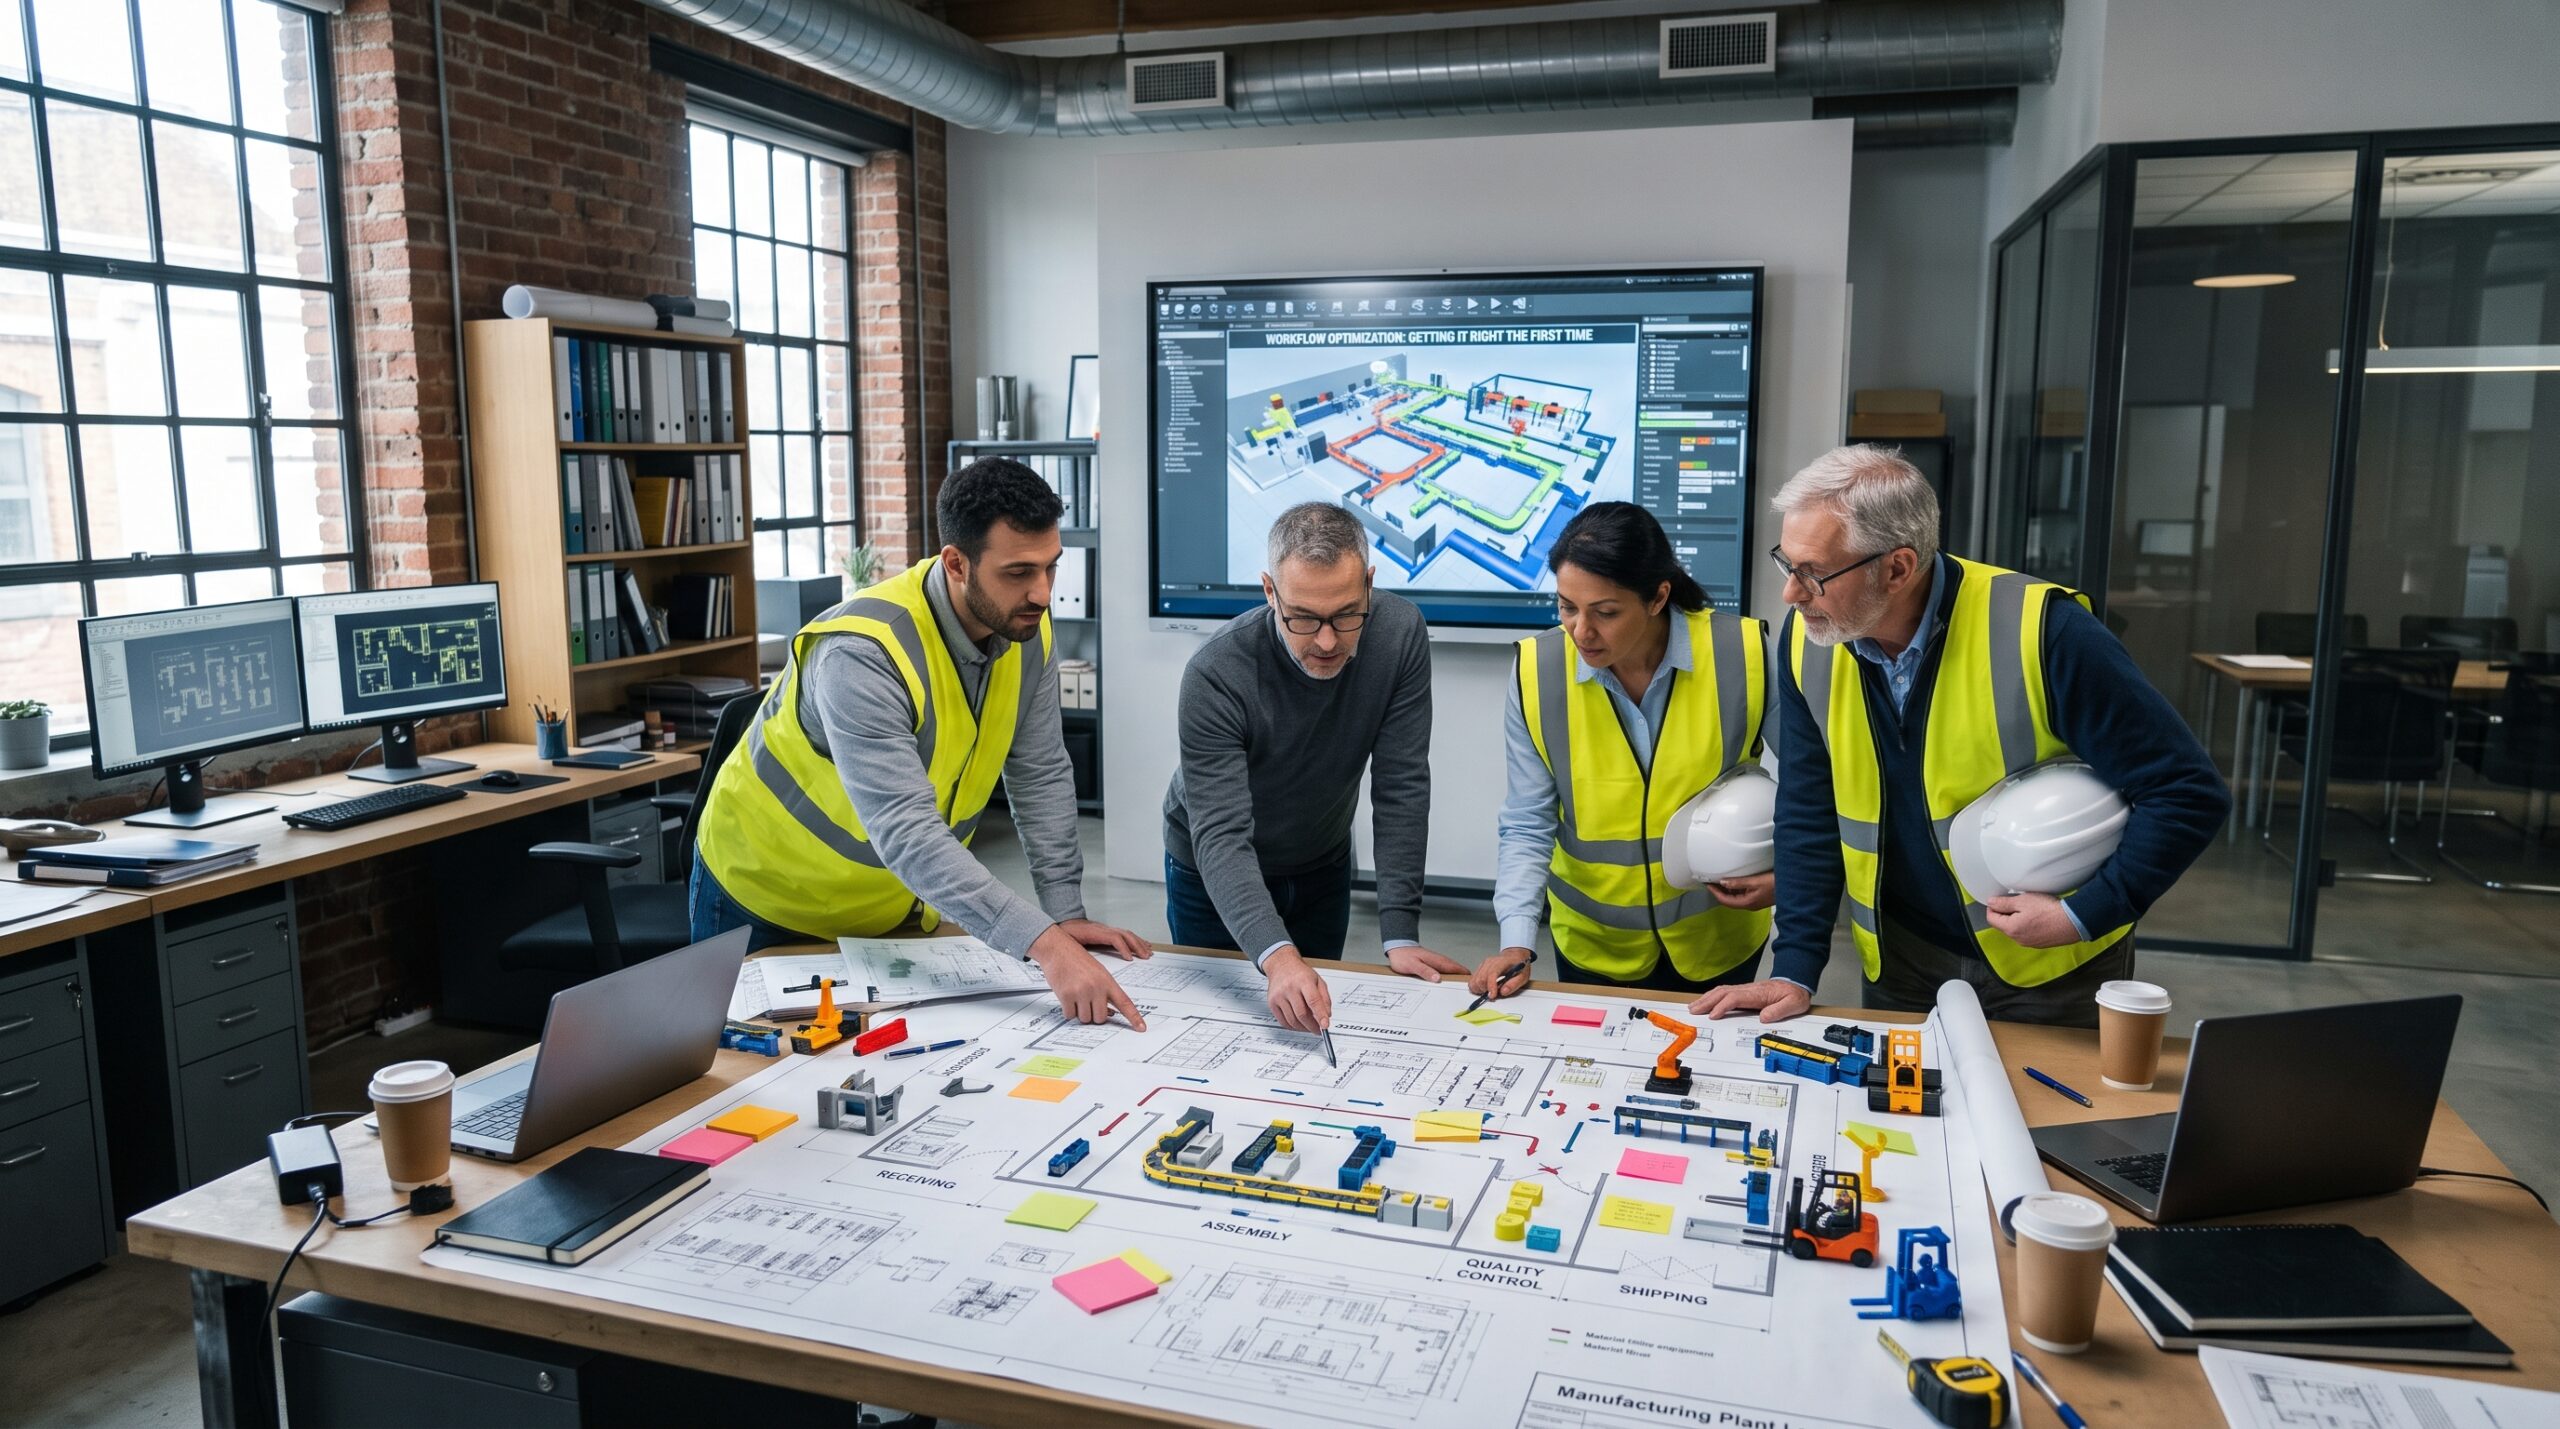
The most expensive line in any manufacturing plant layout design is the one you have to erase after the anchor bolts go in. I learned that early. In my second year out of school, I worked on a stamping and assembly building where the press line had been placed by whoever got to the CAD file first. At first glance, the presses looked great on paper, lined up neatly along the north wall. However, six months after startup, we were moving coils across the entire building with two forklifts running nearly full time, because the coil storage sat at the opposite end from the first press. In short, nobody had drawn the flow. Instead, they had drawn the equipment.
That project taught me what I now tell every client before we pick up a pencil: manufacturing plant layout design is not about where the machines go. Rather, it is about how the work moves. If you get the movement right, the machines almost place themselves. On the other hand, if you get it wrong, you will pay for that mistake every shift, in travel, in waiting, in damaged parts and in tired people, for as long as the building stands.
For that reason, this article walks through how I approach a layout, the analysis I insist on before anyone draws a wall, and the mistakes I keep seeing in plants that “just need a little rearranging.” So if you are planning a new facility, an expansion, or a major rearrangement of an existing floor, this is the thinking that saves you from doing it twice.
Why Manufacturing Plant Layout Design Decisions Outlive Almost Everything Else
Equipment gets replaced. Similarly, software gets upgraded, and product lines come and go. But the building, the column grid, the dock positions, the floor pits, the main utility runs and the crane rails tend to stay put for decades.
The team at Richard Muther and Associates, who carry on the work of the man often called the father of systematic planning, put it plainly in their training material: in most plants and warehouses, layout is the most important part of the facilities plan, because it drives material handling cost, has a major effect on flow times, and determines how well the facility adapts when the product mix changes. In addition, they warn against letting a layout become the accidental result of a string of uncoordinated improvement events. In fact, I have seen that warning come true more times than I can count. For example, ten years of small kaizen moves, each sensible on its own, can leave a plant with a material path that looks like someone dropped a ball of yarn down the stairs.
So when people ask me how much analysis a layout needs, my answer is simple. After all, you are making a decision you will live with for twenty years. Therefore, spend the weeks.
Start Your Manufacturing Plant Layout Design With the Product, Not the Floor
Every layout I have done well started with the same set of questions, and none of them were about square footage. Specifically, Muther’s Systematic Layout Planning (SLP) method frames the inputs as P, Q, R, S and T:
- P is Product. What are you making? Also, what does it weigh, how big is it, how fragile is it, does it need to stay clean, and does it get hot?
- Q is Quantity. How many of each, per day, per week, per year? Just as important, how is that volume distributed across the product family?
- R is Routing. What is the sequence of operations for each product? Furthermore, which steps are shared and which are unique?
- S is Supporting services. Maintenance, tool rooms, quality labs, offices, break rooms, washrooms, compressed air, chillers and waste handling all count here.
- T is Timing. When does the volume arrive, how fast must the product move, and what does the next five years of demand look like?
Read the Volume Curve Before Anything Else
Of those five, the one that changes my recommendation most often is the product and quantity analysis. First, I plot every product or product family by annual volume, highest to lowest. Typically, what comes out is a curve where a small number of parts make up most of the volume and a long tail of parts each run occasionally.
That curve tells you what kind of layout you need. For instance, high volume, low variety products want a dedicated line where work flows in a straight sequence. In contrast, low volume, high variety products usually belong in a process layout, where similar machines sit together and jobs travel between departments. Meanwhile, the middle of the curve is where manufacturing cells earn their keep. As a result, most real plants end up as a hybrid, and that is fine, as long as the hybrid is designed on purpose.
I once worked with a valve manufacturer that wanted one big assembly line for everything. However, their volume curve showed three product families carried 70 percent of the volume, while everything else was a scattering of custom orders. Consequently, we built two flow lines for the high runners and a flexible job shop area for the rest. Had we forced everything onto one line, the changeovers alone would have eaten the capacity they were trying to gain.
Map the Flow First in Manufacturing Plant Layout Design
Once I understand the products, I measure how material actually moves. Unfortunately, this is the part people want to skip, even though it is the part that matters most.
Build a From To Chart
A from to chart is a simple matrix. Every department or work area is listed down the side and across the top. Then, in each cell, you record how much material moves from one area to another over a period of time. I prefer to count moves in equivalent loads, not just trips, because a forklift carrying one tote and a forklift carrying a full pallet are not the same burden.
When the chart is done, a few cells always jump out. Those are your heavy flows, and therefore the areas connected by them need to sit next to each other. That sounds obvious. Still, in nearly every existing plant I have audited, at least one of the heaviest flows runs between two areas that sit far apart, usually because one of them was added later wherever there was room.
Walk It and Draw the Spaghetti
Data from the system only tells part of the story. That is why I always follow the parts and the people with a pen and a floor plan. The Lean Enterprise Institute describes the spaghetti chart as a plot of the path a product takes as it travels through the steps of a value stream. Moreover, they have shared a good example from a thruster builder whose assembly area was transformed after the team simply drew what was happening. Generally, the first time a plant manager sees their own spaghetti chart, the room goes quiet. There are lines crossing back over themselves, operators walking to a shared tool crib forty times a shift, and finished goods traveling past raw material receiving on the way to shipping.
Do this for the operators too, not just the product. Although the walking an operator does to fetch parts, find a gauge or get a signoff is invisible on a routing sheet, it is very visible on the clock.
Score the Relationships That Have Nothing to Do With Flow
Not every reason two areas should be close or apart is about moving material. For this reason, Muther developed the relationship chart. Each pair of activities gets a closeness rating, from absolutely necessary to undesirable, along with a reason code. For example, the paint booth should be far from welding. Likewise, the quality lab should be near final inspection, and the maintenance shop should be close to the equipment that breaks down most often. Shipping and receiving, meanwhile, might share a dock apron to make use of the same yard, or might need to stay separate for traceability.
When you combine the flow data with the relationship ratings, you finally have the true picture of what needs to be next to what. Above all, that is the foundation of every sound manufacturing plant layout design.
Size the Space Honestly in Your Manufacturing Plant Layout Design
Here is where I see the most optimism in plant planning. Too often, someone measures the footprint of a machine, adds a little walking room, and calls it done.
In reality, a space allowance for a workstation includes the machine itself, the operator zone, the incoming material staging, the outgoing material staging, room for maintenance access with panels open, space for tooling and changeover carts, and clearance for whatever equipment delivers and removes material. In fact, on many machining centers I have planned, the machine is less than half of the space it really needs.
Then there is storage. Work in process does not disappear just because a layout drawing has no place for it. So if you do not plan a home for it, it will find one, usually in an aisle.
I also add growth space by area, not as a single block in the corner. For example, if the plan calls for a 15 percent volume increase in three years, I ask where that increase lands. Usually it lands in two or three specific departments, and consequently those are the ones that need expansion room right beside them.
Choosing a Layout Type in Manufacturing Plant Layout Design
With flow, relationships and space in hand, the layout type becomes a decision you can defend rather than a preference. Here is how I think about the four classic options.
Product and Process Layouts
Product layout (line flow). Equipment is arranged in the order of operations. This is best for stable, high volume products, since material handling is minimal and control is simple. However, the weakness is rigidity: one machine down can stop the line, and a big product change may mean a big rebuild.
Process layout (functional). Like machines are grouped together: all lathes here, all welders there. This works well for high variety and low volume, because equipment use is high and expertise stays concentrated. On the downside, it brings long travel, lots of WIP and long lead times, because jobs bounce from department to department.
Cellular and Fixed Position Layouts
Cellular layout. A small group of different machines is arranged to complete a family of parts, often in a U shape so one or two operators can tend several machines. As a result, cells combine much of the flow of a line with much of the flexibility of a job shop. Even so, they work best when part families are well defined.
Fixed position layout. Here the product stays put, and the people, tools and materials come to it. For instance, ships, aircraft, large presses and big structural assemblies are built this way. Accordingly, the layout challenge is staging and access around the product.
The honest answer for most plants is a mix. For example, machining might run as a process layout feeding several assembly cells, which in turn feed a final packaging line. That is not a compromise. Instead, it is matching the layout to the product mix, area by area.
Draw Manufacturing Plant Layout Design Alternatives, Then Make Them Compete
One of the strongest habits SLP builds is generating more than one option. That is why I always develop at least three block layouts before choosing one. A block layout shows areas as rectangles sized to their space needs and placed according to the relationship diagram, without any equipment detail.
Next, I make the options compete. For each one, I calculate total material handling distance weighted by flow volume, since that is the number most likely to separate a good layout from a bad one. Besides that, I score each option against factors that are harder to count: ease of future expansion, safety, supervision visibility, noise and heat separation, how well it uses the existing building, and how disruptive it will be to install.
Let the Floor Team Score It Too
Bring the people who will run the plant into this scoring. After all, supervisors, maintenance leads, material handlers and quality staff will spot problems in an hour that engineers miss in a week. For example, I once had a block layout that scored best on paper until a forklift driver pointed out that the main aisle crossed the pedestrian path to the cafeteria at exactly the point where loaded trucks would be turning. Fortunately, we adjusted it before it became a near miss report.
Only after an option wins on both the numbers and the judgment calls do I move to detailed layout.
The Detailed Manufacturing Plant Layout Design: Where Good Plans Go to Die
Moving from blocks to equipment is where many solid concepts fall apart, because the details fight back. Here is what I check at this stage.
Aisles and Traffic
OSHA’s material handling standard, 29 CFR 1910.176(a), requires sufficient safe clearance wherever mechanical handling equipment is used, including aisles, loading docks, doorways and turns. In addition, it requires permanent aisles to be marked. The walking and working surfaces rule, 29 CFR 1910.22, also adds that passageways stay clear and orderly. While OSHA does not give one fixed aisle width for every case, an OSHA letter of interpretation has long recommended aisles at least three feet wider than the largest equipment that will use them, or a minimum of four feet.
In practice, I design aisles around the actual truck turning radius with a full load, not the brochure number. I also separate pedestrian walkways from truck lanes with physical barriers wherever the two run side by side for any length. Finally, I keep the main aisles straight wherever I can. A straight aisle is a safer aisle, and in addition it is an aisle people actually use instead of cutting through work areas.
Exit routes, however, deserve their own check. Emergency egress is governed separately, so a storage aisle that looks wide enough can still create an egress problem if racks or staged material creep into the path over time.
Utilities and Fixed Elements
Every machine needs something: power, air, water, drains, exhaust, data. Since pits and heavy foundations are the most permanent things in a plant, I place them where the flow analysis says they belong, and then confirm the building can support them. In other words, if a press needs a pit, that press is not moving next year. So make sure it is in the right spot now.
I also like to run main utility headers along the column lines with drops that can be relocated, rather than burying everything in the slab. Admittedly, it costs a little more up front, but it buys enormous flexibility later.
Workstation Detail
At the station level, the goal is to let the operator do value adding work without reaching, bending, walking or waiting. This means parts presented at the point of use, tools within easy reach, and material replenished from behind or the side so the material handler never has to drive through the operator’s space. Put simply, if a forklift has to weave through a cell to drop totes, the layout still has a problem.
Lighting, noise and heat matter here too. For instance, a station next to a heat treat furnace or under a poor light is a station where quality will drift.
Visual Management
A good layout makes the normal state obvious. To that end, use floor marking for aisles, staging areas, WIP locations and safety zones. Similarly, keep clear sight lines so a supervisor can see the whole cell from one spot, and place andon lights or signals where people can actually see them. As a result, when the layout makes problems visible, people fix them faster.
Future Proofing Your Manufacturing Plant Layout Design
Product mixes change faster than buildings. Indeed, almost every client I have worked with saw their mix shift meaningfully within five years of a major layout project. The ones that handled it well, however, had built in flexibility from the start.
So what does that look like in practice?
- Keep expansion walls clear. Do not put the boiler room, the electrical room or a pit against the wall you will most likely push out.
- Favor movable equipment where you can. For example, set machines on leveling pads instead of grouting them in, and use overhead utility drops and modular conveyors.
- Leave the main spine alone. Design one or two main material aisles that can serve the plant through many rearrangements. That way, departments can shift along the spine without breaking the overall flow.
- Plan docks for growth. Receiving and shipping capacity is often the first bottleneck when volume climbs. Therefore, rough in extra dock positions even if you do not equip them yet.
Of course, flexibility is not free. It usually costs some space and some upfront money. Nevertheless, it is far cheaper than tearing out foundations.
Digital Tools Help Manufacturing Plant Layout Design, but They Are Not the Method
Today’s planning tools are excellent. CAD models and 3D views let everyone see the layout before it exists. Likewise, simulation software can model queues, bottlenecks and forklift traffic, and point cloud scans of an existing building catch the column that is two feet from where the old drawing says it is.
I use all of these. However, I have also seen beautiful 3D models of layouts that did not work, because nobody did the flow analysis first. The software makes it easy to drag machines around until the picture looks good. But a good looking picture is not the goal. Instead, short, simple, logical flow is the goal. So do the systematic analysis first, and then use the tools to test and communicate it. Simulation earns its cost when you have variability, shared resources or complex material handling, because that is where intuition fails.
Common Manufacturing Plant Layout Design Mistakes
After enough projects, patterns emerge. These are the ones that cost plants the most.
Planning Mistakes
Placing equipment before mapping flow. The stamping plant from my early career is the classic example. Although the machines fit, the work did not.
Ignoring the support functions. Tool cribs, maintenance, quality labs and offices often get whatever space is left. As a result, operators walk across the plant to get a gauge, and maintenance techs spend half their shift in transit.
Underestimating staging and WIP space. If the drawing has no home for material between operations, then the aisles become that home.
Designing for average volume. Plants must survive their peak months. Therefore, size critical areas, especially receiving and shipping, for realistic peaks, not annual averages.
Safety and People Mistakes
Mixing forklifts and people without separation. This is a safety issue first and an efficiency issue second. So separate them by design, not by signs alone.
Skipping the people who do the work. Operators and material handlers know where the friction is. Consequently, involve them in the alternatives and the detailed review.
Treating the layout as finished at startup. Every layout needs a follow up. For this reason, I plan a review a few months after startup and again after the first year to see where reality has drifted from the plan.
Installation: Protecting Your Manufacturing Plant Layout Design on Its Way to the Floor
Even a great layout can fail during installation. For example, contractors move equipment a few feet to avoid a drain. Similarly, someone sets a rack in an aisle “temporarily,” or a utility drop ends up on the wrong side of a machine.
On every project now, I walk the floor with the installation crew at each major stage and compare it against the approved drawing. In addition, I sequence the move so that the plant keeps shipping. For rearrangements in operating plants, that usually means building inventory ahead, moving in phases over weekends or shutdowns, and having a clear plan for each phase’s temporary flow. After all, rushing a move to save a weekend can cost far more in a messy startup.
After the move, train everyone on the new flow, mark the floor before production starts, and then redo the spaghetti chart within the first month. Ultimately, the before and after comparison is the best proof that the design worked. Moreover, it often reveals one or two small adjustments worth making while everything is still fresh.
A Simple Way to Remember Manufacturing Plant Layout Design
If you take nothing else from this article, take this sequence:
- First, understand the products, volumes and routings.
- Next, measure the flow and score the relationships.
- Then, size the space honestly, including staging, access and growth.
- After that, choose layout types area by area based on the data.
- Develop several block alternatives and make them compete.
- Detail the winner with real aisles, utilities and workstations.
- Finally, install carefully, then measure again.
That is the heart of manufacturing plant layout design done right the first time. Admittedly, it is not glamorous work. Most of it happens on spreadsheets, floor plans and long walks behind a forklift. Even so, it is the difference between a plant that fights you every day and one that quietly does what it was built to do.
Manufacturing Plant Layout Design FAQs
What is manufacturing plant layout design?
Manufacturing plant layout design is the planned arrangement of equipment, workstations, storage, aisles and support areas so that material, people and information move through production with the least wasted effort. Today, Richard Muther’s Systematic Layout Planning method remains the most widely used structured approach.
What are the main types of plant layout?
The four classic types are product (line) layout, process (functional) layout, cellular layout and fixed position layout. In practice, most plants combine them. This plant layout guide from Oxmaint also covers how volume and variety drive the choice.
How wide should aisles be in a manufacturing plant?
OSHA requires sufficient safe clearance where mechanical handling equipment operates and requires permanent aisles to be marked under 29 CFR 1910.176. In addition, an OSHA interpretation letter recommends at least three feet wider than the largest equipment, or a minimum of four feet, as summarized by EHS Daily Advisor.
What is a spaghetti chart used for in layout planning?
A spaghetti chart traces the actual path of a product or person through a process, thereby exposing excess travel and backtracking. For a practical example, the Lean Enterprise Institute shares how one drove major improvement.
How often should a plant layout be reviewed?
Review it whenever new products, equipment or major volume changes arrive, and otherwise at least once a year. For instance, Faber Infinite Consulting recommends an annual assessment as a baseline.
What software is used for factory layout design?
CAD tools are standard for 2D and 3D layout models, while simulation software is used to test flow and capacity before installation. For an overview of common tools and techniques, see Katana.
References
- Richard Muther and Associates. Current Texts and Videos: Systematic Layout Planning (SLP)
- Richard Muther and Associates. About Our Layout and Space Planning Courses
- Richard Muther and Associates. Systematic Planning Methods
- Wikipedia. Richard Muther (industrial engineer)
- Occupational Safety and Health Administration. 29 CFR 1910.176, Handling Materials, General
- Occupational Safety and Health Administration. 29 CFR 1910.22, Walking Working Surfaces, General Requirements
- EHS Daily Advisor. Q&A: Pedestrian Travel Paths
- J. J. Keller Compliance Network. Optimizing Safety: The Importance of Understanding Aisle Width in Your Facility
- Lean Enterprise Institute. Small Chart, Big Impact: How a Simple Spaghetti Chart Led to Huge Wins at Thrustmaster of Texas
- Oxmaint. Best Practices for Manufacturing Plant Layout Design: A Complete Guide
- Katana. Optimize Your Factory With a Production Layout Guide
- Faber Infinite Consulting. Factory Layout Planning: Step by Step Guide to Improve Workflow